Intralogistic Conveyor Solutions: Improving Material Handling Efficiency in Modern Industries
-
- September 18th, 2026
- 35 views
In today's competitive manufacturing and logistics environment, businesses are continuously looking for ways to improve operational efficiency, reduce material handling costs, and increase productivity. Intralogistic conveyor solutions play a critical role in automating the movement of materials, products, cases, bags, crates, and pallets across manufacturing facilities, warehouses, and distribution centers.
Manual material handling can lead to operational delays, higher labor requirements, product damage, and inconsistent workflows. By integrating automated conveyor systems into industrial operations, businesses can achieve smoother material flow, improved workplace safety, and better production efficiency.
Alligator Automations India Pvt. Ltd. provides industrial automation and material handling solutions designed to support the evolving requirements of manufacturing and logistics industries.
What Are Intralogistic Conveyor Solutions?
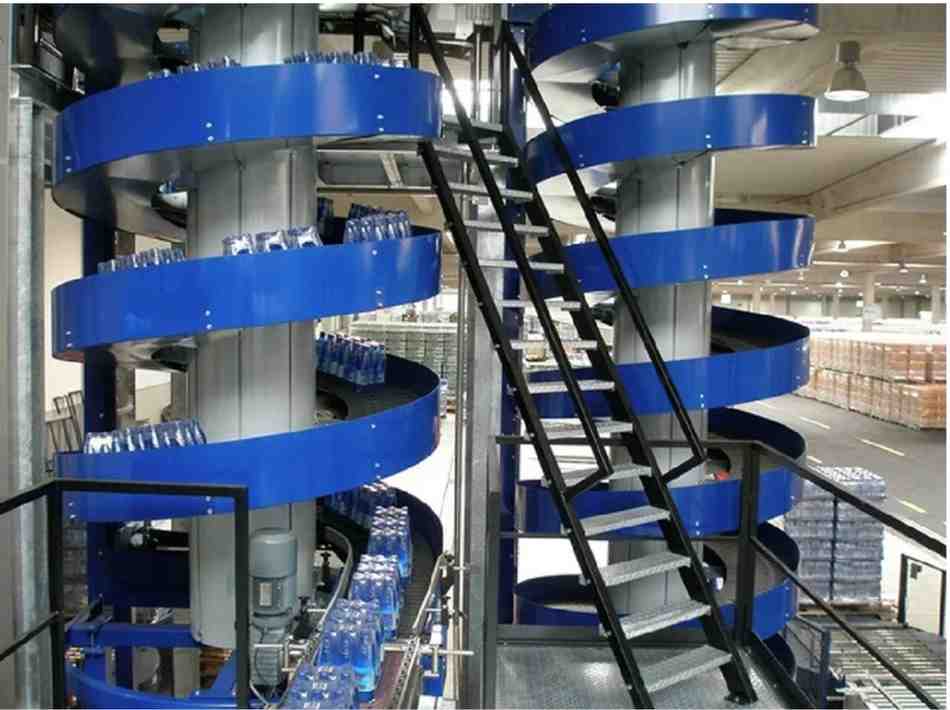
Intralogistic conveyor solutions are automated material transportation systems used to move products and materials within a facility. These systems connect different stages of manufacturing, packaging, storage, and dispatch, helping businesses streamline internal logistics operations.
Depending on the application, conveyor systems can be designed to handle:
- Industrial pallets and heavy loads
- Tyres and wheels
- Product cases, bags, and crates
- Packaged goods
- Materials for warehouse and production line operations
A well-designed intralogistics system helps optimize material flow while supporting integration with other industrial automation equipment.
Why Are Intralogistic Conveyor Systems Important for B2B Industries?
Manufacturing and logistics businesses require dependable material handling systems that can support continuous operations and changing production demands.
Modern conveyor solutions offer several potential benefits:
1. Improved Material Handling Efficiency
Automated conveyors reduce unnecessary manual transportation between workstations, production lines, and storage areas. This helps create a more organized material flow and supports efficient plant operations.
2. Reduced Manual Handling
Conveyor automation minimizes repetitive carrying and movement of materials. Depending on the application, this can improve workplace ergonomics and allow employees to focus on other operational tasks.
3. Better Production Workflow
Conveyors can connect multiple process stages, including packaging, inspection, storage, and dispatch. Properly integrated systems help reduce unnecessary movement and support consistent operations.
4. Scalable Industrial Solutions
Modular conveyor designs can be adapted to different plant layouts, load requirements, and production processes. Businesses can select suitable conveyor configurations based on their operational needs.
5. Integration with Industrial Automation
Conveyor systems can be integrated with sensors, control systems, robotic equipment, and other automation technologies to support coordinated material movement.
Types of Intralogistic Conveyor Solutions Offered by Alligator Automations
Alligator Automations provides a range of conveyor solutions for different industrial material handling applications.
1. Tyre Handling Solutions
The tyre manufacturing industry requires specialized material handling systems for the movement of tyres and wheels across various production and processing stages.
Tyre handling conveyor solutions can support:
- Tyre movement between production processes
- Automated material transportation
- Improved workflow organization
- Integration with industrial handling systems
2. Pallet Conveyor Systems
Pallet conveyor systems are designed to transport heavy and palletized loads across manufacturing plants, warehouses, and distribution facilities.
These systems can be used in applications involving:
- Pallet transportation
- Production line integration
- Warehouse material movement
- Automated loading and unloading processes
- Pallet transfer and accumulation
Depending on the project requirements, conveyor configurations may include roller conveyors, chain-driven systems, transfer units, and other pallet handling technologies.
3. Product Handling for Cases, Bags, and Crates
Cases, bags, and crates are commonly used for packaging and transporting products across industrial facilities. Efficient product handling systems help move these units between processing, storage, and dispatch operations.
Automated case, bag, and crate conveyors can support:
- Internal product transportation
- Packaging line integration
- Material flow between workstations
- Warehouse handling applications
- Reduced repetitive manual movement
The conveyor design should be selected according to product dimensions, weight, packaging type, speed, and operating conditions.
4. Roller Conveyor Systems
Roller conveyor systems are widely used for industrial material handling, particularly when transporting cartons, containers, pallets, and other unit loads.
Roller conveyor solutions can be configured for different operational requirements, including:
- Product transportation
- Pallet handling
- Workstation integration
- Material accumulation
- Warehouse logistics
Factors such as load weight, roller diameter, conveyor width, operating speed, and layout influence the selection of an appropriate roller conveyor system.
5. Belt Conveyor Systems
Belt conveyors are used for transporting a wide range of products and materials across manufacturing and packaging operations.
They can be suitable for applications involving packaged products, cases, and other materials requiring continuous belt-supported transportation.
Key considerations when selecting a belt conveyor include:
- Product characteristics
- Conveyor length and width
- Required transportation speed
- Load capacity
- Integration with existing machinery
- Operational and maintenance requirements
Industries That Benefit from Intralogistic Conveyor Automation
Intralogistic conveyor systems can be used across multiple industries where efficient internal material transportation is important.
Automotive and Tyre Manufacturing
Conveyor systems support the movement of tyres, components, and production materials across manufacturing processes.
Food and Beverage
Material handling solutions can support the transportation of packaged products, cases, and containers in suitable production and distribution environments.
Cement and Industrial Manufacturing
Heavy-duty conveyor systems can be used for handling industrial products and materials, depending on load specifications and operating conditions.
Warehousing and Distribution
Conveyors help connect warehouse processes such as product movement, accumulation, sorting, and dispatch.
Packaging Industries
Conveyor systems support the transfer of packaged products between packaging machines, inspection stations, and dispatch areas.
How to Select the Right Intralogistic Conveyor System
Selecting the right conveyor system requires a detailed understanding of your facility's material handling requirements.
Businesses should consider the following factors:
1. Product and Load Specifications
Evaluate product dimensions, weight, packaging type, and handling characteristics.
2. Production Capacity
Determine the required throughput and operating speed to match the production process.
3. Plant Layout
Review available floor space, conveyor routing, transfer points, and integration with existing machinery.
4. Automation Requirements
Identify whether the system needs sensors, PLC controls, robotic integration, accumulation, or other automated functions.
5. Safety and Maintenance
Consider guarding, emergency stops, accessibility, maintenance requirements, and operational safety.
6. Future Expansion
Select a system design that can accommodate potential changes in production capacity or facility requirements.
Why Partner with Alligator Automations?
Alligator Automations India Pvt. Ltd. focuses on industrial automation and material handling solutions for businesses seeking to improve their manufacturing and logistics operations.
Our conveyor solution portfolio covers tyre handling, pallet conveyor systems, case/bag/crate handling, roller conveyors, and belt conveyor systems.
With project-specific engineering and automation integration, businesses can explore conveyor configurations aligned with their operational requirements.
The right solution depends on your application, load characteristics, production workflow, and facility layout.
Intralogistic conveyor solutions are an important part of modern industrial material handling. From tyre manufacturing and pallet transportation to product handling and packaging operations, automated conveyors can help businesses create organized and efficient internal material flow.
Choosing the right conveyor system requires careful evaluation of operational requirements, product specifications, throughput, safety, and integration needs.